Outlook on Laser Welding Trends in Industrial Manufacturing
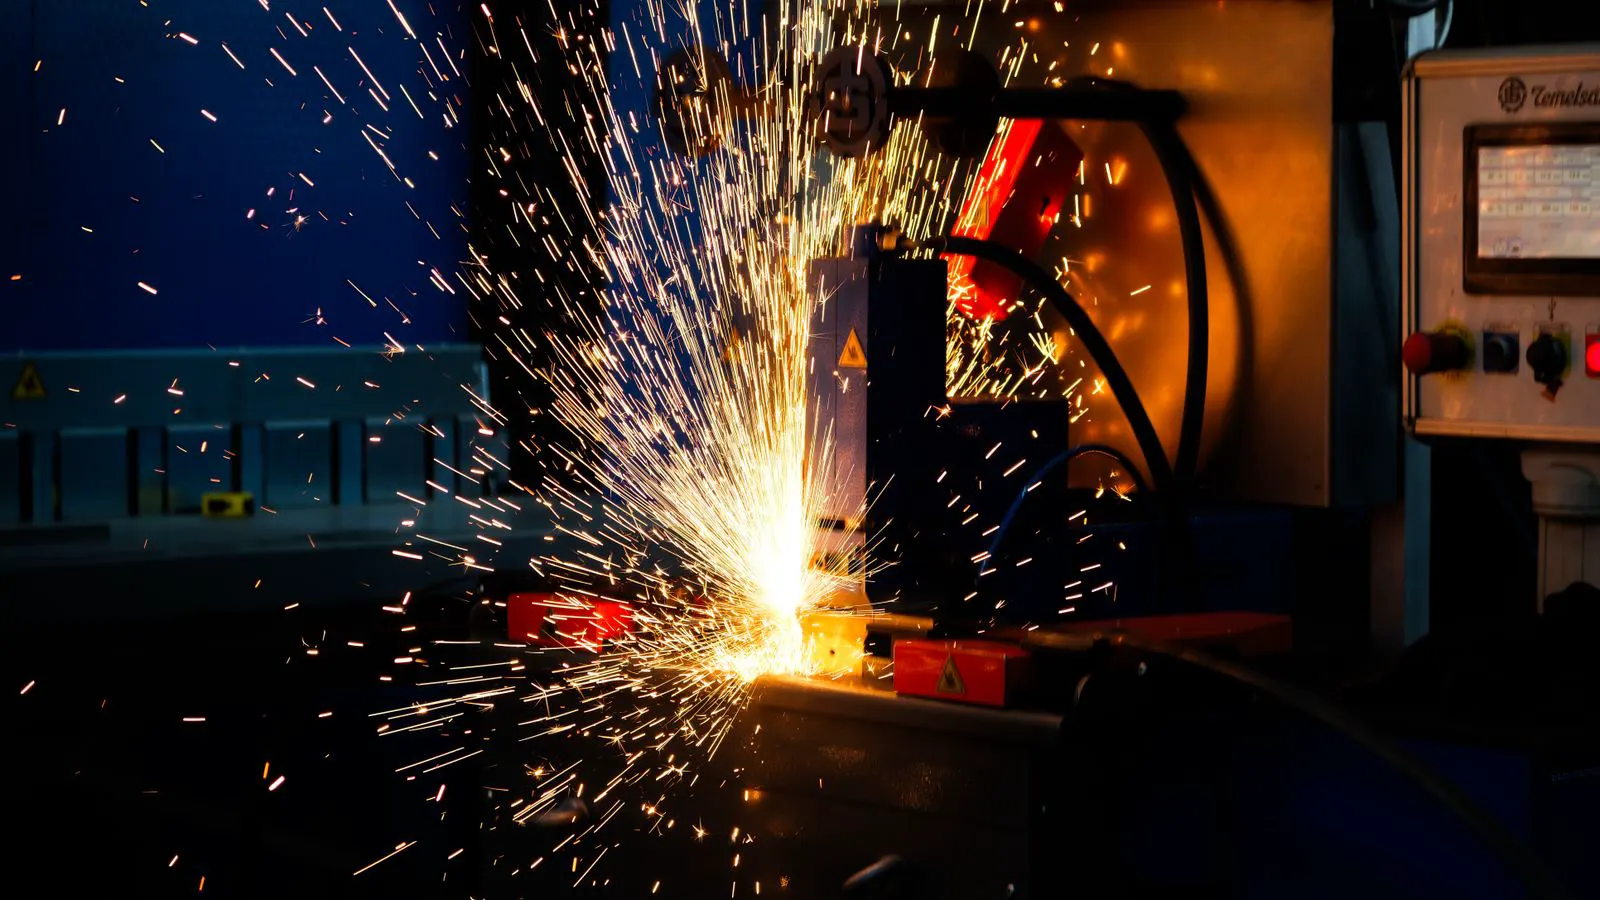
Laser welding is moving toward higher precision, flexible automation, and tighter integration with production data. Buyers should prepare for systems that handle diverse materials faster and require less manual intervention.
- High power fiber systems are pushing into thicker materials while keeping heat affected zones small.
- Automation and vision systems are becoming standard for repeatable weld quality.
- Material handling and fixturing are changing to support faster cycle times.
- Data integration is moving from optional to expected in modern production lines.
- Buyers should plan for flexibility in power output and control software.
Where industrial laser welding is heading
Laser welding is shifting from a manual or semi-automated process to a more integrated part of the production line. The machines are getting faster and more capable of handling different materials without major setup changes. For buyers, this means the value of a laser welding system is expanding beyond the weld itself. It now includes setup time, repeatability, and how well the machine fits into the rest of the workflow.
The change is visible in how plants are structuring their welding cells. A few years ago, a laser welder was often a standalone unit operated by a technician who made many manual adjustments. Now, the machine is expected to run with less human input. The operator monitors the process, but the system handles much of the parameter control.
This shift affects purchasing decisions. A buyer looking at industrial laser welding should not only evaluate the laser source. They should also look at the control system, the fixture design, and the ability to store and recall weld programs. The machine is no longer just a heat source. It is a production tool that must fit into a larger process.
How power and material capability are expanding
Fiber laser sources are the dominant platform for most industrial laser welding applications. The trend is toward systems that can cover a wider range of material thicknesses and alloys. A single machine may handle thin sheet steel, stainless steel, aluminum, and mild steel with the same basic setup.
This capability matters for plants that do not run a single material all day. If a production line switches between parts made from different materials, a flexible welder reduces changeover time. The laser does not need to be swapped out for each material. The operator adjusts the power, the beam profile, and the shielding gas flow.
However, higher power is not the only factor. A welder that can put out high energy but cannot control that energy well will create defects. The trend is toward better beam quality and more precise control of the pulse width and repetition rate. This allows the machine to make a strong weld in a small area without melting the surrounding material.
The result is a narrower heat affected zone. For thin sheet, this is a major advantage. The part does not warp. The surrounding area does not discolor. The weld does not require as much post processing. For thicker material, the same principle applies. The weld penetrates deeper without a wide pool of melted metal.
How automation and vision are changing the process
The second major shift is the integration of vision systems and automated positioning. A laser welder now often includes cameras and sensors that check part position before the weld starts. The system can detect if a part is shifted by a few millimeters and adjust the laser head accordingly.
This is not new technology, but it is becoming standard. Buyers who used to rely on manual jigs are now looking for machines that can compensate for small errors automatically. The difference is in repeatability. A manual setup might produce a good weld, but the next part may be slightly off. A vision-guided system keeps the weld point consistent every time.
This is especially important for small batch production. In high volume, a jig can hold parts in place. In small batch work, the parts vary more. The machine needs to adapt. The trend is toward cells that can handle more variety without a full retooling.
The automation does not stop at positioning. Some systems now include automatic clamping and part loading. The operator places the part on a fixture, and the machine does the rest. This reduces the number of people needed at the weld station. It also makes the process safer. The operator is not standing over the beam while the weld happens.
How data and connectivity are moving into the shop floor
The third shift is the integration of welding data with the plant management system. Each weld now has a record. The system stores the parameters used, the power level, the gas flow, and the duration of the weld. This data can be pulled out for quality checks or for training new operators.
This is not just about quality. It is about process control. If a weld fails, the operator can look at the data and see what was different. Was the power too high? Was the gas flow low? Was the part position off? The data makes the problem visible. Without it, the operator is guessing.
For buyers, this changes the evaluation of a laser welding system. The software interface matters. The system should be easy to use and easy to maintain. If the data is locked in a system that is hard to access, the value drops. The machine should be able to send weld data to a central server or a cloud platform.
This also affects maintenance. The system can track usage hours and flag when a component needs service. For example, the laser head or the nozzle may need cleaning after a certain number of hours. The system can remind the operator before a failure happens. This reduces downtime and extends the life of the machine.
How fixture design and material handling are adapting
The fourth shift is in how parts are held during welding. Traditional welding fixtures are heavy and designed for a specific part. The trend is toward modular fixtures that can be reconfigured for different parts. This supports the flexibility that modern production lines need.
Modular fixtures use quick-connect clamps and adjustable plates. The operator can change the fixture in minutes instead of hours. This is important when the production schedule changes. If a new part comes in, the weld station can be adapted without waiting for a new fixture.
The material handling also changes. Instead of carrying parts by hand, plants use conveyor systems or robotic arms to move parts between stations. The laser welder becomes one station in a line. The part moves from cutting to welding to inspection. The laser welder does not sit alone in the room.
This integration has a cost implication. A simple laser welder is cheaper to buy. A full welding cell with automation, vision, and data integration costs more. But the cost per weld may be lower. The labor time is reduced. The rework time is lower. The setup time is shorter.
For buyers, the decision is not just about the laser machine. It is about the whole cell. The fixture, the controls, and the integration all affect the return on investment. A buyer should ask how the machine will fit into the current layout. If the shop floor is tight, a large automated cell may not fit. In that case, a smaller, more flexible system may be the better choice.
How material knowledge is changing the buying process
The fifth shift is in the level of material knowledge required. Laser welding is not a one-size-fits-all process. Each material behaves differently under the beam. Aluminum reflects more laser energy than steel. Stainless steel discolors easily. Mild steel is forgiving but requires more heat to penetrate.
Buyers are no longer just looking at the laser power. They are asking about beam quality, pulse control, and the ability to work with different alloys. The machine should have presets for common materials. The operator should be able to select aluminum and have the system adjust the parameters automatically.
This knowledge also affects the choice of shielding gas. Different materials need different gas mixes. Argon is common for aluminum. Nitrogen is used for stainless steel. The machine should be able to switch gas types or use a gas mixer. This reduces the need for manual adjustments.
The training of operators is also changing. A new operator needs to understand not just how to press the button, but why the parameters are set that way. The machine should have clear feedback. If the weld is not good, the system should show what needs to be adjusted. This reduces the learning curve and lowers the risk of defects.
How to prepare for these changes
The final point is how a buyer should prepare. The first step is to look at the current production workflow. What materials are being welded? What is the volume? How often do the parts change? The answer to these questions determines the type of system needed.
If the plant runs a single material in high volume, a simple, high power laser welder may be enough. The focus should be on speed and reliability. If the plant runs multiple materials in small batches, the focus should be on flexibility. The machine should be able to switch quickly and adapt to different parts.
The second step is to evaluate the integration. How will the machine connect to the rest of the line? Will it need a vision system? Will it need to send data to a central server? The answer to these questions determines the software and control requirements.
The third step is to consider the long term. The market is moving toward more automation and more data. A buyer should choose a system that can grow with the business. If the plant adds more parts or increases volume, the system should be able to handle it.
The fourth step is to talk to the supplier about support. The machine will need maintenance and updates. The supplier should be able to provide training and technical support. The cost of the machine is only part of the total cost of ownership. The support and service are equally important.
The last step is to test the machine on real parts. A demo on a standard test piece is not enough. The buyer should bring their own material and run a weld. The operator should check the quality, the speed, and the ease of setup. This gives a clear picture of how the machine will perform in the actual environment.
The changes in laser welding are not happening overnight. But the direction is clear. The machines are getting smarter, more flexible, and more integrated. Buyers who plan for these changes will be in a better position to adopt the technology. Buyers who only look at the laser power will miss the bigger picture.
The goal is not to buy the most expensive machine. The goal is to buy the right machine for the current and future needs of the plant. The trends in laser welding are about making the process more efficient, more repeatable, and more integrated. The buyer who understands this will make a better decision.
Frequently asked questions
What is the biggest change in laser welding over the last few years?
The biggest change is the integration of vision systems and data logging into standard welding cells. This reduces manual setup and improves repeatability.
Do I need a high power laser for thin sheet?
No. High power is useful for thick material. For thin sheet, beam quality and control matter more than raw power. A lower power machine with good control can produce a better weld.
How do I know if a laser welder is flexible enough for my plant?
Look at the number of presets, the ability to switch gas types, and the speed of parameter changes. If the machine can handle multiple materials with quick adjustments, it is flexible enough.
Is automation worth the extra cost?
It depends on the production volume. For high volume, automation reduces labor cost and increases repeatability. For small batch work, a semi-automated system may be enough.
What should I check during a demo?
Bring your own material and run a weld. Check the quality, the setup time, and the feedback from the system. This gives a clear picture of how the machine will perform in your environment.