How to Set CO2 Laser Speed and Power for Thick Wood
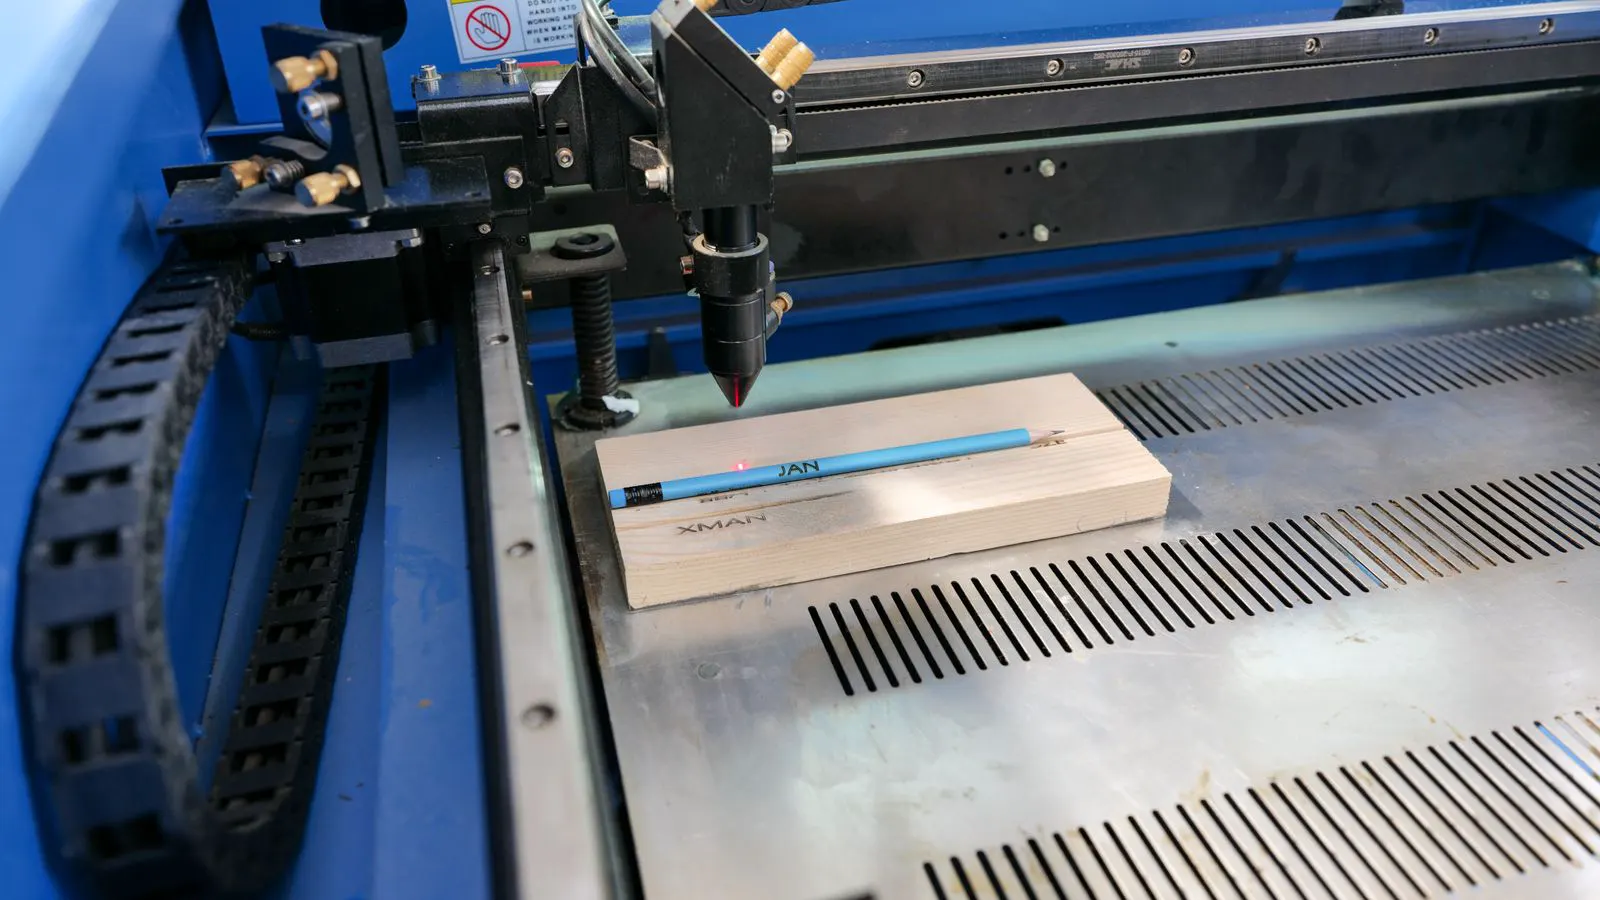
To cut thick wood cleanly with a CO2 laser, start with a high power and low speed, then reduce speed gradually while monitoring kerf width and edge quality. Use consistent material thickness, stable focus, and a high gas flow to keep the cut clean.
- Start with the highest power and a slow speed, then increase speed until the cut breaks through cleanly.
- Keep the material thickness uniform and the focus ring locked before running a full cut.
- Use a high assist gas flow to clear the kerf and prevent burnt, rough edges.
- Watch the edge color and kerf width; both are direct indicators of whether speed or power needs adjustment.
What to check before you set any parameters
Thick wood behaves differently from thin sheets. The density, grain direction, and moisture content all change how fast the beam has to travel. Before touching the control panel, confirm the material is stable. A board that is still moving as it dries will not cut straight. Check the thickness with a caliper, not just the nominal size. A half-millimeter difference across the board can change the cut time and edge quality. Measure at three points, at least. If the board bows, the beam will focus on one side and leave the other side charred.
Look at the grain. Cutting with the grain is generally faster and cleaner. Cutting across the grain slows the process and can create jagged edges. If the wood is a veneer or a composite, the top layer may burn before the core is cut through. That creates a stepped kerf and weakens the final part. Check for knots and voids. Dense knots require more energy to cut, while soft spots may burn through too quickly. A consistent density across the board ensures a uniform cut.
How to find the starting power and speed
Do not start at a low power. Low power leaves a dark, carbonized edge and can clog the kerf with char. Start at the maximum power your machine allows. Set a modest speed, low enough that the beam has time to heat the material fully. Run a single test line across a scrap piece of the same wood. Use a scrap that matches the board in species and moisture content.
Watch what happens at the end of the line. If the board only melts at the surface and does not break through, the speed is too slow or the power is too low. If the line burns a deep channel but does not cut all the way through, increase the power. If the cut is through but the edges are dark and rough, the speed is too slow. The goal is a clean break, not a melted channel.
Adjust one variable at a time. Change the speed in small steps. After each change, run a new test line. This is how you find the balance point. Keep a notebook or a digital log. Note the power, speed, and gas flow for each test. This data helps you repeat the process on future boards.
How to read the kerf and edge quality
The kerf is the width of the cut. A clean cut on thick wood should have a narrow, consistent gap. If the kerf is very wide, the material is burning away around the beam path. That usually means the speed is too slow. If the kerf is narrow but the edges are dark, the beam is not moving fast enough to keep the char from building up.
Look at the top and bottom edges separately. The top edge is exposed to the beam first. If it is charred while the bottom edge is clean, the power is too high or the speed is too low. If the bottom edge is charred but the top is clean, the beam is losing focus or the gas flow is not clearing the kerf evenly.
The edge color gives you a quick read. A light tan edge means the wood is cutting cleanly. A dark brown or black edge means the material is burning. A grey or ashy edge means the char is not being cleared by the gas. Check the edge under good light. Shadows can hide defects that are visible in bright light.
How to set the assist gas flow
Assist gas is not optional on thick wood. It clears the molten material from the kerf and cools the edges. Too little gas and the cut clogs with char. Too much gas and it can push the beam off center or create a wide, messy kerf.
Set the gas flow to a medium-high level for the first test. If the edges are rough and dark, increase the flow. If the kerf is wide or the edge is uneven, reduce the flow. The goal is a steady stream that clears the kerf without disturbing the cut path. Use air or nitrogen, depending on your machine’s capability. Nitrogen often produces a cleaner edge on thick hardwoods because it does not introduce oxygen that can cause further burning.
Step-by-step parameter setup for thick wood
- Load the material and confirm the thickness. Use a caliper and measure at several points. Uneven thickness changes the cut time and can break the part.
- Set the focus ring to the recommended position for your board thickness. A wrong focus spreads the beam and burns the edges.
- Start at maximum power. Set a low speed that gives the beam time to cut. Run a test line.
- Increase the speed in small steps. Run a test line after each change. Watch the kerf width and edge color.
- Adjust the assist gas flow. Increase it if the edges are charred. Reduce it if the kerf is wide or uneven.
- Run a full test cut on a scrap piece. Check the part for warping, delamination, or stepped edges.
- Fine-tune the power if the cut is clean but slow. A slight reduction in power can speed up the process without hurting quality.
Common mistakes that ruin thick wood cuts
Starting with a low power is the most common error. It creates a burnt channel and wastes time. Another mistake is changing both speed and power at the same time. When you change two variables, you cannot tell which one caused the change in quality.
Ignoring the grain direction is another issue. Cutting across the grain on thick hardwoods often produces a rough edge and a long cut time. If you must cut across the grain, reduce the speed further and watch the edge. The grain pulls against the beam, creating a resistive force that slows the cut.
Not cleaning the material before cutting is a simple but costly mistake. Dust and finish on the wood absorb the beam and cause uneven heating. A quick wipe with a clean cloth before the cut can make a visible difference. Also, check for resin pockets. These can burn and clog the gas flow, creating a wide kerf.
How to verify the final parameters
Run a full test part on the actual material. Check the cut edges under good light. Run your finger along the edge to feel for burrs or roughness. A clean cut should feel smooth with no raised fibers. If the edge is rough, slow the speed down or increase the gas flow.
Measure the kerf width with a caliper. Compare it to the width on a thin piece of the same wood. A consistent kerf across the board means the parameters are stable. If the kerf changes along the cut, check the focus and the material thickness.
Save the final settings in your machine software. Label the file with the material type, thickness, grain direction, and power-speed pair. This saves time when you run the same board again. Use a standardized naming convention. For example, “Oak_15mm_WithGrain_100P_120S”.
Quick reference for typical parameter ranges
| Material thickness | Power | Speed | Gas flow |
|---|---|---|---|
| 6 to 10 mm | 70 to 90 percent | 200 to 400 mm/min | Medium |
| 10 to 15 mm | 85 to 100 percent | 100 to 250 mm/min | Medium-high |
| 15 to 25 mm | 100 percent | 50 to 150 mm/min | High |
| 25 mm and above | 100 percent | 30 to 100 mm/min | High |
These ranges are starting points. The grain direction, species, and moisture content will shift the actual numbers. Use the test line method to find the exact point for your material.
Frequently asked questions
Can I cut thick wood with low power and a very slow speed?
Low power and a slow speed will burn the wood instead of cutting it. The char builds up and clogs the kerf, producing a rough, dark edge and a long cut time.
How do I know if my focus is set correctly for thick wood?
Run a test line. If the edges are wide and charred, the beam is out of focus. Adjust the focus ring until the kerf narrows and the edge color lightens.
Should I cut with or against the grain?
Cutting with the grain is faster and cleaner. Cutting against the grain requires a slower speed and a higher gas flow to keep the edges from tearing.
What if the cut is through but the edges are black?
Black edges mean the material is burning. Increase the speed or reduce the power. Run a new test line after each change to see the effect.
Can I use the same settings for oak and pine?
No. Different species have different densities and burn rates. Always run a test line on the specific wood you are cutting before starting a production run.