How to Select Laser Protective Eyewear for Operators
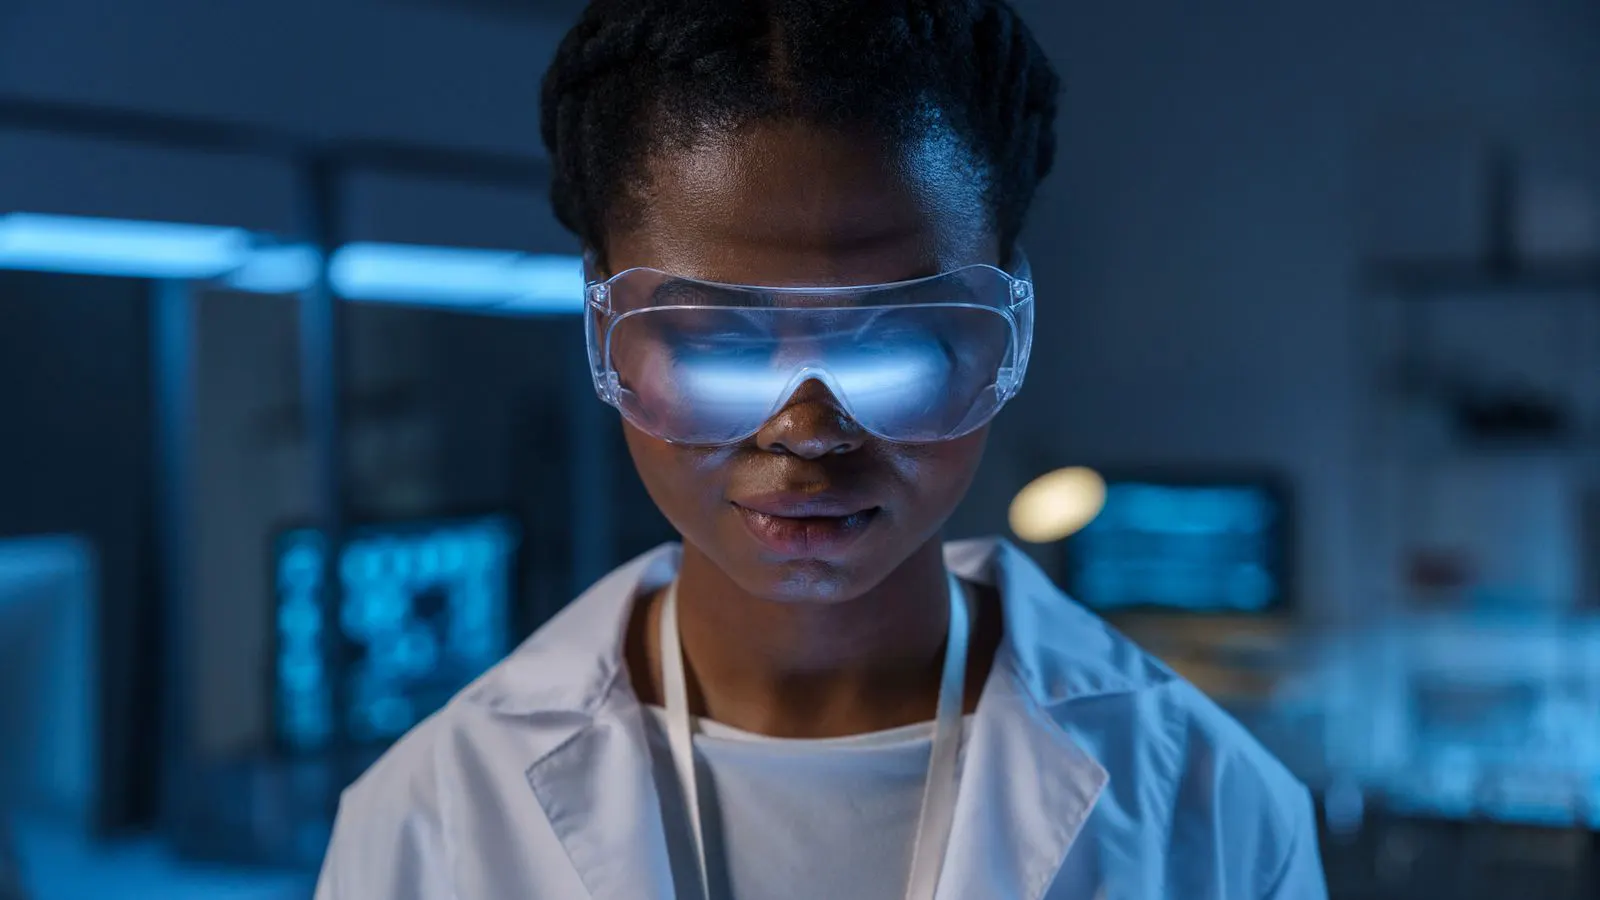
Selecting laser protective eyewear requires matching optical density to the laser wavelength, beam class, and expected exposure. This guide walks through the technical steps to ensure operators have the correct category and type of laser safety glasses for their specific machine environment.
- Always verify the optical density rating against the specific laser wavelength, not just the class.
- Check the OD values at both the center and edge of the lens for non-uniform coatings.
- Ensure the eyewear is rated for the beam class and the specific exposure duration of the task.
- Match the frame and lens shape to the operator's face and the machine's enclosure design.
- Keep a log of eyewear inspections and replace lenses if scratched or degraded.
Why Generic Laser Safety Glasses Fail in Industrial Settings
Operators often reach for the same pair of safety glasses for every machine on the line. This habit creates a gap between the protection the machine requires and what the operator actually wears. A CO2 laser at 10.6 micrometers and a fiber laser at 1.06 micrometers emit radiation that interacts with the eye very differently. The lens material, coating, and optical density must align with the specific emission.
The primary failure mode is not a sudden accident but a cumulative mismatch. An operator might wear eyewear rated for visible light but exposed to an infrared beam that the lens passes without significant attenuation. The eye receives the full energy, even if the beam is invisible. Industrial environments add complexity. Multiple machines, varying power levels, and open work cells increase the chance of exposure outside the primary beam path.
This article focuses on the technical selection process. It assumes you have already identified the laser parameters. If you need to verify class, wavelength, and power, start with the laser safety standards and compliance checklist before buying equipment. The steps below ensure the eyewear matches the machine reality, not just the label.
Step 1: Confirm the Laser Wavelength and Power
Start with the machine data plate or the operator manual. You need the exact wavelength in micrometers, the peak power, and the average power. Fiber lasers typically operate near 1.06 or 1.07 micrometers. CO2 lasers emit at 10.6 micrometers. Diode lasers vary from 355 to 1064 nanometers. The wavelength determines how the lens material absorbs the energy.
Power dictates the required optical density. A low power diagnostic laser might require a lower OD than a high energy production laser. Do not assume all Class 4 lasers need the same protection. The energy density at the eye level is the deciding factor. If the machine has multiple laser heads or a scanning head, the beam path changes. Identify the worst case scenario where the operator might be exposed.
If the data is missing, measure it. Use a power meter calibrated for the specific wavelength. Do not rely on the manufacturer’s nominal rating if the machine has been modified. Check the interlock status as well. An open interlock might reduce power, but you must plan for the highest possible output during maintenance or setup.
Step 2: Determine the Beam Class and Exposure Duration
The beam class tells you the inherent danger. Class 3B and Class 4 lasers require protection for direct and diffuse beam exposure. Class 3R lasers may require protection for direct beam exposure only. Class 1 and 1M are generally safe for normal use, but protective eyewear is often still required by site policy.
Exposure duration matters as much as class. A short pulse might be safe with lower OD, while a continuous wave beam requires higher attenuation. The task determines the exposure. Spot welding, cutting, and marking have different duty cycles. An operator standing near a cutting cell for thirty minutes faces a different risk profile than someone holding a probe for five seconds.
Write down the task and the expected time. If the operator will be inside the enclosure during maintenance, the exposure is higher. If they are outside the enclosure during normal operation, the exposure is lower but still present. The selection must cover the worst case task you anticipate. Do not select for the average case. Plan for the day the guard is open or the beam is misaligned.
Step 3: Select the Optical Density Based on Wavelength
Optical density, or OD, is the logarithmic measure of attenuation. An OD of 4 blocks 99.99 percent of the light. An OD of 6 blocks 99.9999 percent. The OD must be specified at the laser wavelength. A lens might be OD 4 at 532 nanometers but only OD 2 at 1064 nanometers.
This is where most buyers make mistakes. They see an OD rating and assume it applies to all wavelengths. Check the datasheet carefully. Look for the OD at the specific wavelength of your laser. If the laser has a wavelength shift or a harmonic, check those too. For example, a green diode laser might emit at 532 nanometers but have a weak 1064 nanometer component. The protection must handle the strongest component.
For high power lasers, the OD should be at least 4, often 6. For lower power lasers, OD 4 might suffice. The standard practice is to calculate the required OD based on the accessible dose limit. The accessible dose limit is the maximum energy the eye can receive without harm. Subtract the laser output from this limit to find the required attenuation. The OD must be high enough to bring the exposure below that limit.
Step 4: Check the Lens Material and Coating
Not all materials absorb infrared radiation the same way. Polycarbonate is common but may not be ideal for high energy CO2 beams. Some polycarbonate lenses can be damaged by high power infrared, leading to cracking or delamination. Glass lenses with special coatings often perform better for high power applications.
The coating is critical. The coating must be durable and resistant to thermal damage. If the coating fails, the OD drops instantly. Check the manufacturer’s specifications for thermal stability. The coating should be tested for the specific wavelength and power level. A coating that works for a 100 watt laser might fail on a 1000 watt laser.
Frame material also matters. Metal frames can conduct heat. If the operator is working in a hot environment, the frame should be comfortable and not trap heat. Plastic frames are lighter but may warp. The frame must be secure enough to stay on the face during movement. A loose frame shifts the optical center, reducing protection.
Step 5: Verify the OD at the Edge of the Lens
Laser safety lenses are not always uniform. The coating is often thinnest at the edges. The OD at the edge might be lower than the OD at the center. If the operator looks through the edge of the lens, they receive less protection.
Check the datasheet for the OD at the edge. Some high quality lenses maintain high OD across the entire surface. Others have a gradient. If the lens has a gradient, the operator must be trained to look through the center. This is a practical issue. In a busy workshop, operators might not follow this instruction.
If the edge OD is low, consider a lens with a uniform coating. These cost more but reduce the risk of human error. Also check for scratches. A scratch can scatter the beam and increase local exposure. Inspect the lens before each shift. Replace it if you see any damage. A scratched lens is not just a comfort issue. It is a safety issue.
Step 6: Match the Eyewear to the Machine Environment
The physical fit is as important as the optical rating. If the eyewear is uncomfortable, operators will take it off. Look for frames that fit the operator’s face. Consider the presence of other PPE. If the operator wears a face shield, the eyewear must fit underneath it. If they wear a hard hat, the headband must not interfere.
Consider the machine enclosure. If the operator looks through a small window, the eyewear must fit within that space. If the enclosure is open, the eyewear must be secure against wind or movement. In a cutting cell, the operator might be leaning forward. The eyewear must stay on during this movement.
Test the fit. Have the operator move their head quickly. Does the eyewear shift? Does it leave marks on the nose or ears? If it is uncomfortable, they will remove it. Comfort is a safety feature. Choose a model that the operator likes. Offer options if possible. A standard set of eyewear that fits some people well and others poorly is a liability.
Step 7: Document the Selection and Train the Operator
Once you select the eyewear, document the selection process. Record the laser parameters, the required OD, and the specific model chosen. This creates a paper trail. If an incident occurs, you need to show that you selected the correct protection based on the machine data.
Train the operator on the specific eyewear. Show them the OD rating and why it matters. Explain the wavelength limitation. Tell them what to do if the lens gets scratched. Provide a spare pair. If the primary pair is damaged, the operator should not operate the machine without a replacement.
Keep a log of inspections. Check the lenses monthly or after each major maintenance. Record any damage. Replace lenses when they show signs of wear. Do not wait for a catastrophic failure. A small crack can propagate under stress. Regular inspection is a low cost measure that prevents high cost incidents.
Common Mistakes in Eyewear Selection
The most common mistake is buying based on color. Green or amber lenses look safe. They are not. The color is just the visible light transmission. The infrared absorption is what matters. A green lens might be OD 1 at 1064 nanometers. Do not judge protection by appearance.
Another mistake is assuming one pair fits all lasers. If your facility has fiber, CO2, and diode lasers, you need different eyewear for each. A single pair of eyewear might not cover all wavelengths. Buy separate pairs for each laser type. Label them clearly. Do not mix them up.
The third mistake is ignoring the edge OD. Many operators look through the edge of the lens. If the edge OD is low, they are exposed. Buy lenses with uniform OD. This is more expensive but safer. Do not cut corners here.
Final Verification: The “Would You Wear It?” Test
After selection and training, perform a final check. Put the eyewear on. Look at the laser beam indicator. If there is a visible beam, check for leaks. If the beam is invisible, trust the data. But check the fit. Check the cleanliness. Check the date code if applicable.
Ask the operator: “Is this comfortable? Do you understand why you are wearing this?” If the answer is no, address it. Do not force compliance. Build trust. When the operator understands the risk and the protection, they will wear it consistently.
This verification step is not a formality. It is the last line of defense. The selection process is technical. The verification is practical. Both are required. A perfect datasheet means nothing if the operator takes the glasses off because they hurt.
The goal is simple. Match the OD to the wavelength. Match the fit to the operator. Document the decision. Train the user. Inspect regularly. These steps turn laser protective eyewear from a piece of equipment into a reliable safety control.
Frequently asked questions
Can I use one pair of laser safety glasses for both a fiber laser and a CO2 laser?
No. Fiber and CO2 lasers emit at different wavelengths, and the OD rating is wavelength specific. You need separate pairs rated for each specific wavelength.
What if the laser data plate is missing or faded?
Measure the laser output with a calibrated power meter. Verify the wavelength and power before selecting eyewear. Do not rely on guesswork.
How often should I inspect laser protective eyewear?
Inspect before each shift or at least monthly. Replace lenses immediately if you find scratches, cracks, or delamination. Do not use damaged lenses.
Does the color of the lens matter for safety?
No. Color is irrelevant. Only the optical density at the specific laser wavelength matters. A green lens is not automatically safer than a gray one.
Can I use the same eyewear for Class 3B and Class 4 lasers?
Only if the OD rating is sufficient for the Class 4 laser. Class 4 lasers have higher power. The eyewear must be rated for the higher energy density. Check the OD values.